If you’ve ever stood in a industrial facility’s control room, watching gauges flicker and pipeline pressures adjust in real time, you’ve probably wondered how operators keep every process running at peak efficiency. From our vantage point as a diverter valve supplier, that question isn’t just theoretical—it’s the core of every conversation we have with plant managers, process engineers, and maintenance teams. Diverter valves are often overlooked as “simple” components, but they act as the invisible backbone of countless systems, turning wasted energy, unnecessary downtime, and inconsistent performance into something far more reliable and cost-effective. Today, I want to break down exactly how a diverter valve impacts system efficiency, drawing on the real-world projects we’ve supported over the past decade. Diverter Valve
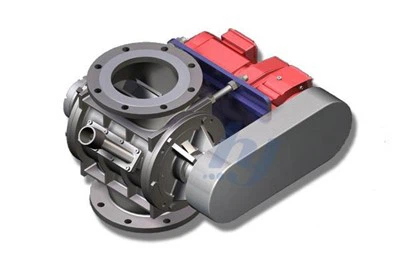
First, let’s ground this in what a diverter valve actually does, because misconceptions here lead to so many avoidable efficiency losses. A diverter valve is a flow control component designed to redirect or split fluid, gas, or slurry streams between two or more outlets, or to mix multiple streams into a single inlet. Unlike a simple gate or ball valve that only opens or closes a line, diverter valves are engineered for precise, repeatable flow changes—critical for systems where even a 1% fluctuation in flow can translate to thousands of dollars in wasted energy or product. I remember a 2021 project with a petrochemical plant in the Midwest that was using standard gate valves to switch product lines between two reactors. Their process required switching every 45 minutes, and every time they opened or closed the gate, it caused a pressure spike that forced their upstream pumps to work 12% harder than necessary to compensate. They were wasting an estimated $18,000 a year on excess pump energy alone, all because their valve couldn’t handle gradual, controlled flow changes. That’s the first big lesson: when a valve is sized, designed, and applied correctly, it eliminates unnecessary load on upstream equipment, directly cutting energy use.
Let’s dive deeper into that energy efficiency angle, because it’s the most tangible impact of diverter valves on system performance. Most industrial systems rely on centrifugal pumps or compressors, which are most efficient when they operate at a steady, design flow rate. Any time flow is interrupted or redirected abruptly, those pumps have to work harder to overcome pressure changes, friction, or line losses. A properly engineered diverter valve mitigates this in two key ways: flow modulation and pressure recovery.
Flow modulation is the ability of a diverter valve to adjust the split or redirection of flow smoothly, without sudden shifts. Take the chemical processing sector, where many plants run multiple batch reactors that require switching feedstocks at different intervals. If you use a valve that has a dead zone (a range of positions where flow doesn’t change) or is prone to cavitation, switching between feed lines means slamming flow from 100% to 0% in a fraction of a second. That not only creates pressure surges but also causes the pump’s impeller to experience sudden changes in velocity, leading to increased wear and reduced efficiency over time. We worked with a specialty chemical manufacturer in Texas a few years ago that was experiencing 15% higher pump energy costs than their industry peers. They had installed a generic diverter valve to switch between two acid feed lines, but the valve’s design meant that when it was 30% open, flow would dribble instead of shifting gradually, forcing the pump to run at an unsteady load to prevent starving the reactor. After we replaced it with a valve designed for seamless, continuous flow modulation, their pump energy dropped by 12%—and they saw a 7% reduction in pump maintenance costs, because the impeller was no longer being subject to the stress of sudden flow changes.
Pressure recovery is another often-overlooked factor. When fluid flows through any piping system, it loses energy to friction, and any obstruction in the line will create additional pressure drop. The design of a diverter valve’s internal geometry directly impacts how much pressure is lost when flow is redirected. For example, a simple two-way diverter valve that uses a linear plug to split flow will create more turbulence than a valve with a streamlined, contoured disc. That turbulence translates to unnecessary pressure drop, which means the upstream pump has to generate more head (pressure) to maintain the required flow, burning more energy. We recently tested this with a food and beverage client that uses diverter valves to switch between milk processing lines for regular and chocolate milk. They were using a valve that caused a 2.2 psi pressure drop when switching lines, requiring their feed pump to run at 1,500 RPM instead of the ideal 1,300 RPM. We installed a contoured-seal diverter valve that reduced that pressure drop to 0.4 psi, allowing them to run the pump at its optimal speed. The result? They cut their monthly electricity costs for that pump by 8%, and the pump’s service life extended by an estimated two years, because it wasn’t operating outside its design range.
Beyond energy use, diverter valves drive efficiency through process consistency and reduced downtime—two factors that are often harder to quantify than energy costs but have a massive impact on overall system productivity. No system runs at peak efficiency if it’s experiencing unplanned shutdowns, or if product quality fluctuates because of inconsistent flow. Diverter valves play a key role here by enabling automated, repeatable process steps that eliminate human error.
Consider water and wastewater treatment plants, which rely on diverter valves to direct flow between treatment stages: raw water intake, coagulation, filtration, and disinfection. In a typical plant, if a diverter valve malfunctions, flow can bypass a filtration stage, leading to poor water quality that requires reprocessing—wasting water, chemicals, and energy. We had a client in Florida that was experiencing an average of two unplanned shutdowns per month due to valve failures in their secondary treatment lines. Each shutdown cost them roughly $22,000 in lost production and emergency repairs. The valves they were using were not rated for the cyclic loading of 10,000+ switches per year, so their seals and actuators wore out quickly. When we worked with them to specify heavy-duty diverter valves with self-lubricating seals and robust actuators, they reduced unplanned shutdowns to less than one per quarter. That improvement in uptime directly boosted their system efficiency by cutting lost production, reducing chemical waste from reprocessing, and allowing their treatment stages to operate at a steady, designed flow rate.
Process consistency is equally critical for industries like pharmaceuticals, where even a small variation in flow can ruin a batch of high-value medication. We support several biotech facilities that use diverter valves to switch between different reagent lines during drug formulation. A valve that can’t maintain precise flow rates during a switch can cause a batch to have incorrect reagent concentrations, leading to thousands of dollars in scrap. One of our clients, a biotech firm in Massachusetts, was seeing a 3% batch rejection rate due to flow inconsistencies during line switches. They switched to our precision-engineered multi-port diverter valves, which are calibrated to maintain flow within 0.5% of the setpoint during redirection. Within six months, their batch rejection rate dropped to 0.2%, saving them over $500,000 annually in raw materials and production time. That’s the kind of efficiency gain that doesn’t show up on energy bills, but it’s often the difference between a system that meets its production targets and one that runs at a loss.
Another area where diverter valves drive efficiency is in waste reduction, particularly for industries that handle high-value or hazardous materials. When a system is designed to waste less fluid or gas during flow changes, it’s inherently more efficient. For example, in the natural gas industry, compressor stations use diverter valves to redirect gas between pipelines during maintenance or to match demand fluctuations. Older diverter valve designs would vent small amounts of gas to atmosphere during switching, not only wasting product but also contributing to greenhouse gas emissions. Modern zero-leak diverter valves, which use metal-sealed or soft-sealed designs that eliminate fugitive emissions, have changed that. We worked with a compressor station in Pennsylvania that was venting an average of 12,000 cubic feet of natural gas per day during line switches. After upgrading to zero-leak diverter valves, they eliminated that venting, saving them over $140,000 per year in lost gas revenue and helping them meet strict emissions regulations. That’s a double win: efficiency for their bottom line, and efficiency for environmental performance.
Of course, none of this is to say that all diverter valves improve efficiency—poorly specified or installed valves can actually hurt performance. I’ve seen plants that use a diverter valve designed for gas flow in a slurry application, leading to seal damage, flow blockages, and higher maintenance costs. The key to unlocking the efficiency benefits of a diverter valve is matching the valve’s design to the specific application: fluid type, pressure and temperature ranges, required switch frequency, and flow accuracy. That’s why we don’t just sell valves—we work with clients to conduct a system audit, map their flow requirements, and recommend a valve that fits their exact needs, not a one-size-fits-all option.
For example, a mining client in Nevada was using a general-purpose diverter valve to switch slurry lines for ore processing. The slurry contained abrasive particles that were wearing down the valve’s internal components in six months, requiring frequent replacements that caused downtime and waste. We recommended a diverter valve with a hard-faced internal liner and a robust actuator, designed to handle abrasive slurries. The valve’s wear life extended to three years, cutting their annual valve replacement costs by 75% and reducing downtime associated with valve swaps by 80%. That’s a clear example of how matching the right diverter valve to the application turns a source of inefficiency into a long-term efficiency driver.
As we look to the future of industrial efficiency, diverter valves will only become more important. With increasing pressure to reduce energy use, cut waste, and meet emissions targets, every component of a system has to work as efficiently as possible. Diverter valves, once seen as a afterthought, are now recognized as critical points where efficiency can be unlocked at scale. Whether it’s a small manufacturing line or a large petrochemical complex, a well-designed diverter valve can deliver returns that far exceed the initial investment—often paying for itself in a matter of months through energy savings, reduced downtime, and lower waste.

If your team is looking to identify inefficiencies in your process system, or if you’re ready to upgrade your valves to boost performance, we’d be glad to partner with you. Our engineers have worked across dozens of industries, from food and beverage to oil and gas, pharmaceuticals to water treatment, and we have the expertise to recommend a solution tailored to your unique needs. Let’s start a conversation to find out how a diverter valve can help your system run more efficiently, reliably, and profitably.
Gravity Diverter Valve References
- G. B. Wallis, “One-Dimensional Two-Phase Flow,” McGraw-Hill, 1969.
- American Water Works Association, “Water Treatment Plant Design,” 5th ed., McGraw-Hill, 2012.
- Fluid Controls Institute, “Valve Selection and Application Guide,” 3rd ed., CRC Press, 2018.
- U.S. Department of Energy, “Industrial Pump Systems: Energy Efficiency Opportunity Assessment,” 2020.
- International Society of Automation, “Process Valve Handbook,” 2nd ed., ISA, 2015.
Shanghai Hanye Engineering Technology Co., Ltd.
As one of the most experienced diverter valve manufacturers and suppliers in China, we offer a wide range of products with superior quality. We warmly welcome you to buy customized diverter valve at competitive price from our factory. For more information, contact us now.
Address: Building 7, No. 428 Banqiao East Road, Shanyang Town, Jinshan District, Shanghai
E-mail: Windy@hanye-tech.com
WebSite: https://www.hanyeconveying.com/
